Computer vision has quietly become one of the most practical automation technologies available. Not because models got dramatically better, but because the cost of running them collapsed — inspection that once required a dedicated industrial vision system now runs on a module costing a fraction as much.
That shift changed which problems are worth solving. Tasks too small to justify automation five years ago are now straightforward, and the limiting factor has moved from capability to whether a business case exists.
This guide covers where computer vision genuinely pays, how to tell a suitable problem from an unsuitable one, and what it costs to run in production. For the engineering of building it into a device, see our guide to embedded computer vision.
Where Computer Vision Earns Its Place
Inspection and quality control
Surface defects, missing components, label accuracy, fill levels, dimensional checks. Vision inspects every unit rather than a sample, consistently, at line speed, with an image attached to each result for later dispute.
The value is usually not catching more defects than a human — it is catching them at a consistent rate on the night shift, in hour seven, on unit forty thousand.
Counting and flow measurement
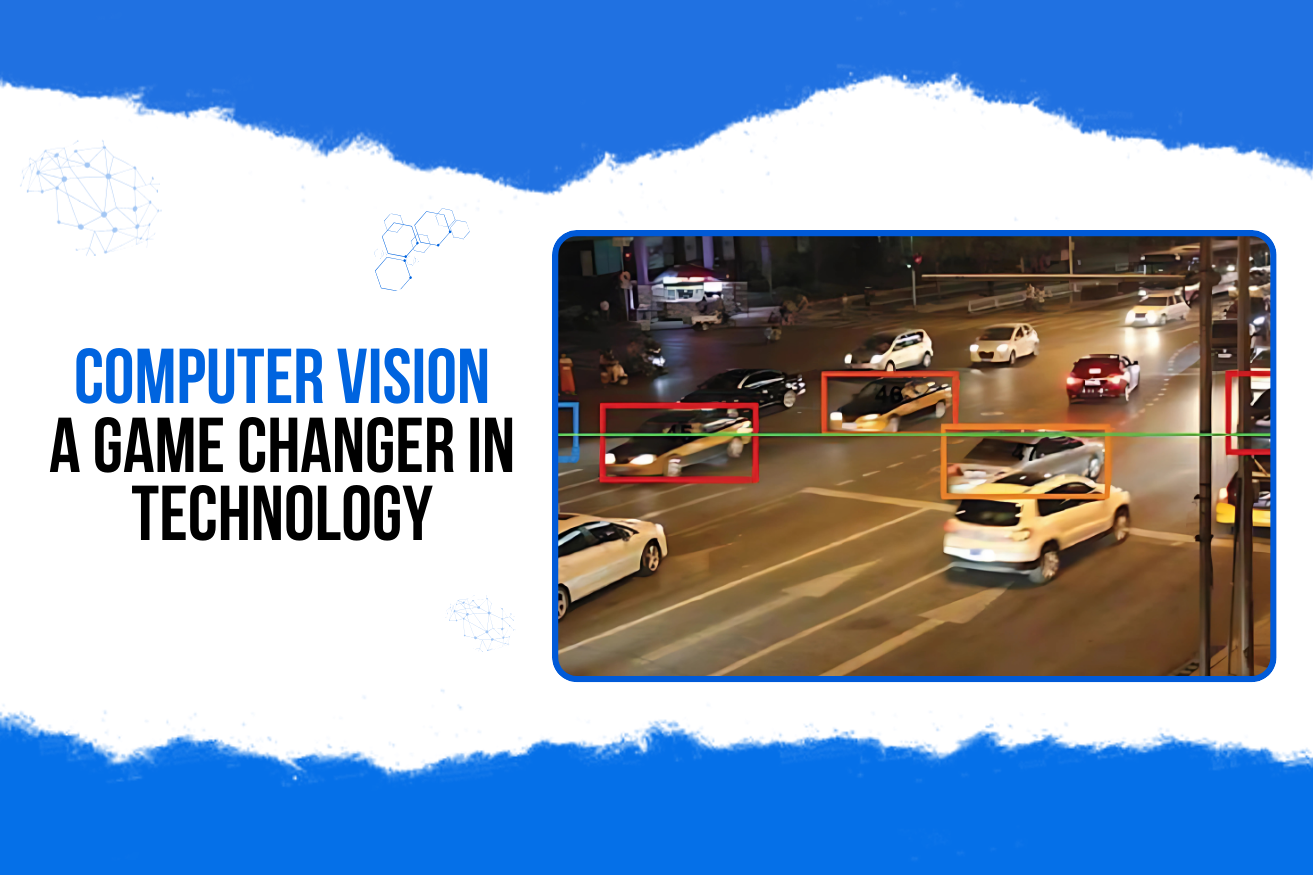
People through an entrance, vehicles in a yard, items on a conveyor, stock on a shelf. These are among the most reliable vision applications because the question is simple and the answer is a number that feeds directly into operations.
Safety and compliance monitoring
Protective equipment checks, exclusion zone breaches, blocked fire exits. Continuous monitoring catches what periodic audits miss, and the record matters as much as the alert.
Reading what humans read
Serial numbers, labels, gauges, barcodes in poor condition. Vision bridges analogue equipment and digital systems without replacing the equipment — often the cheapest way to get data out of machinery too old to have a network interface.
Guidance and robotics
Pick-point detection, alignment, obstacle avoidance. Here vision is a closed-loop input rather than a reporting tool, which raises the reliability requirement considerably.
Which Problems Are Actually Suitable
The success rate of vision projects depends far more on problem selection than on technology. These characteristics separate the two.
| Likely to succeed | Likely to disappoint |
|---|---|
| The defect is visible to a person in a photo | Experts disagree about what counts as a defect |
| Lighting can be controlled or added | Scene lit by changing daylight |
| Object position is reasonably constrained | Objects appear at any angle, scale and overlap |
| A few well-defined categories | Open-ended “detect anything unusual” |
| Hundreds of labelled examples obtainable | Defect occurs twice a year |
| Occasional errors are tolerable | A single miss is a safety event |
If two experienced inspectors disagree about an image, a model will not resolve the disagreement — it will reproduce it inconsistently.
That last point is the most common reason inspection projects stall. Before collecting any data, have two people independently label the same hundred images. If they agree on only 80 percent, that number is your realistic accuracy ceiling, and the first task is defining the standard rather than training a model.
What It Actually Costs to Run
Hardware is rarely the main expense. Three other costs dominate and are routinely underestimated.
- Labelled data. Collecting and annotating representative images across conditions, shifts and seasons is usually the largest single cost, and it recurs whenever the process changes.
- Lighting and mounting. Controlled illumination, fixtures, and enclosures are modest in price and decisive in accuracy. Skimping here costs far more in model effort later.
- Ongoing maintenance. Lenses get dirty, cameras drift, products change appearance, and seasons alter ambient light. Accuracy declines gradually with no error raised, so monitoring and periodic retraining are permanent obligations.
A vision system should therefore be budgeted like a piece of equipment with a service interval, not like a software purchase.
Running a Vision Project That Works
Frequently Asked Questions
Conclusion
Computer vision became a practical automation tool when the cost of running it fell far enough that modest problems became worth solving. The technology is no longer the constraint.
What decides outcomes now is problem selection and discipline: pick tasks a person can do from a single image, define the standard before collecting data, fix the optics before the model, decide how errors should be distributed, and monitor image quality so silent degradation is caught. Projects run that way succeed routinely; those that start with the model rarely do.